Open Solder Joints: How AOI Detects Visible Defects
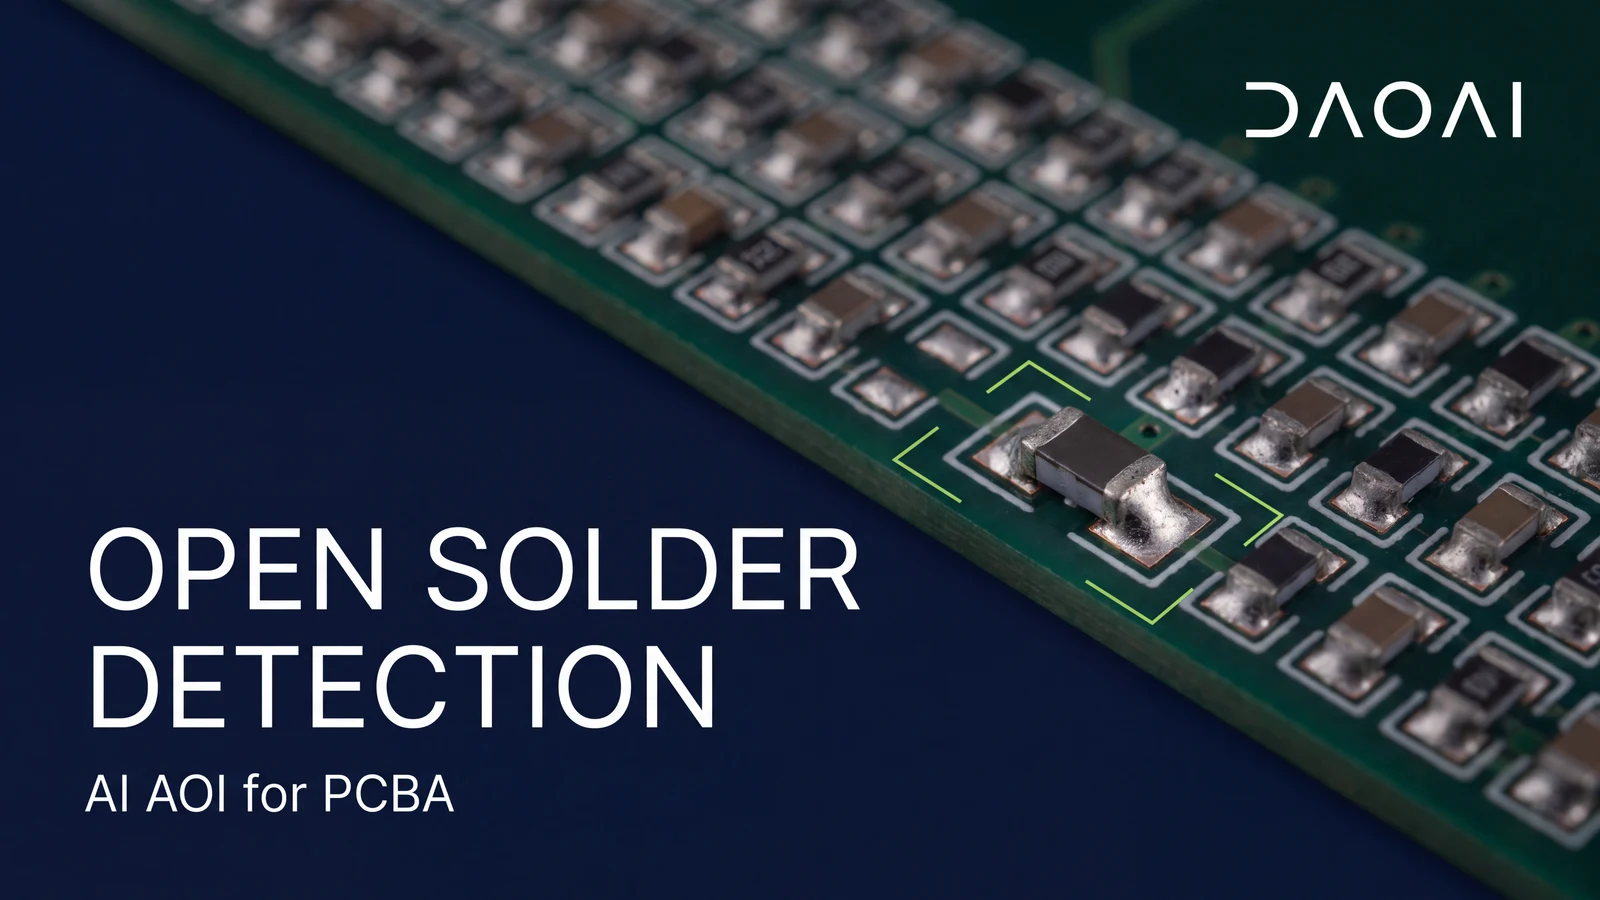
See how AOI identifies visible open solder joints, where fixed color thresholds struggle, and how a pretrained 2D model handles common and special cases.
September 17, 2026
Specs are the entry ticket. The real differences on a high-mix floor: programming inputs, changeover time, and false-call burden. Seven questions expose them.
To choose an AOI for high-mix PCB assembly, weight recurring costs over one-time specs. Camera resolution and board handling matter, but every serious vendor clears that bar. What separates systems on a high-mix floor is what each changeover costs you: which inputs programming requires, who can run it, how long it takes, and whether false calls fall on their own or have to be tuned down again after every new lot.
Most AOI buying guides walk you through resolution, lighting, and board sizes, then stop. Useful, and incomplete. A machine you reprogram three times a week is a different purchase from a machine you program twice a year, even if the two share a spec sheet. This guide covers the requirements audit, the offline versus inline decision, the 2D versus 3D question, and seven questions that expose how a system will actually behave after the honeymoon.
For high-mix production, the selection criteria that matter most are the recurring ones: programming input requirements (CAD files, component libraries, or a physical golden board), changeover time per new job, whether an operator or a dedicated engineer runs it, and how false calls are controlled over time. Hardware specs still set the floor, but they are paid for once. Changeover economics get paid every week.
Think of the spec sheet as the entry ticket. Resolution to see your smallest package, board size range, conveyor compatibility: any credible machine on your shortlist will pass, and the vendors know it, which is why the demo leans on those numbers.
The weight flip happens on your floor, not in the spec sheet. At one new job a month, programming effort is a rounding error. At three NPIs a week per line, programming effort becomes the dominant line item in the machine's five-year cost, ahead of the purchase price. The programming workflow and the false-call burden are where that cost lives, and they deserve the same scrutiny a buyer normally reserves for optics.
Before comparing machines, audit your own line. Count NPIs per line per week, typical lot size, and how often CAD data is actually available when a job lands. Note who would run changeovers (a dedicated AOI engineer or line operators), the current false-call and re-inspection burden, and whether your takt requires inline gating or a bench-side offline unit covers it. These answers set the weights for every criterion that follows.
Six questions, answered honestly, will do it:
Write the six answers down. They turn vendor conversations from adjective exchanges into checkable claims.
Offline AOI fits high-mix, low-volume production: it programs and inspects without stopping the line, tolerates irregular job flow, and costs less to deploy. Inline AOI earns its premium on stable, high-throughput lines where boards must be inspected at takt, every pass, with conveyor integration and automated reject handling. The deciding factors are takt requirement and changeover frequency, not equipment prestige.
A practical mapping:
| Your situation | Better fit | What to verify in a demo |
|---|---|---|
| High-mix, low-volume, frequent NPI | Offline | Programming time on a board you brought, run by your operator |
| Upgrading from manual visual inspection | Offline | Ramp-up time for operators with no AOI background |
| Stable product, single lane, inspection at takt | Inline | Cycle time per board at your panel size, conveyor handoff |
| High-volume, throughput is the constraint | Inline, dual-lane | Sustained throughput with both lanes live, reject handling |
| Mixed reality: NPI bench plus volume lines | Both, offline for NPI | Whether programs transfer between offline and inline units |
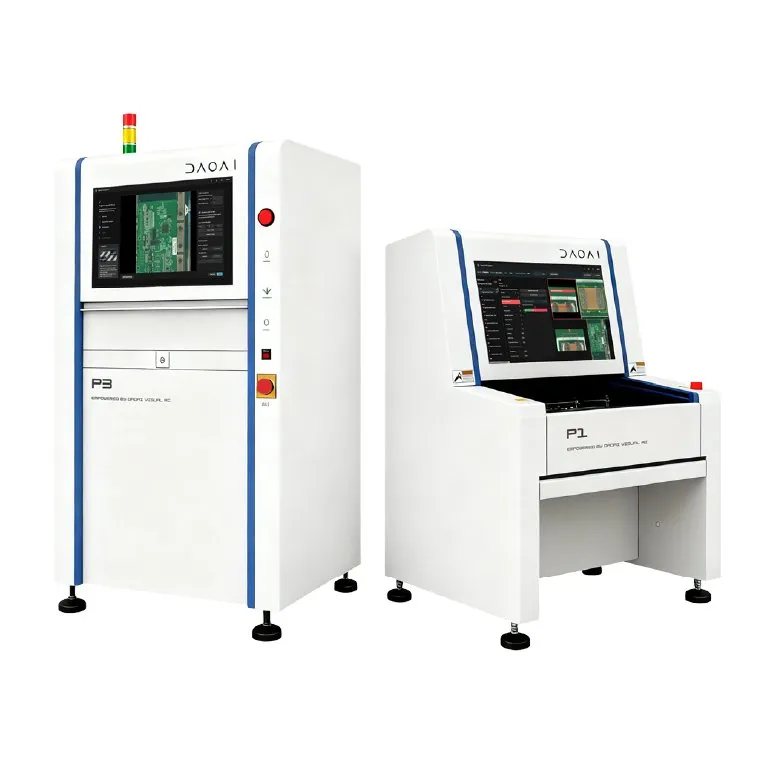
Two honest notes. First, plenty of high-mix shops run entirely on offline units and never miss inline. Second, the both-worlds pattern is common at scale: program and validate offline while production runs, then load the proven program to the inline machine. DaoAI's P Series follows this split, with offline P1 and high-precision P2 (12MP, 10 micron optics for fine-pitch work), and inline P3 plus dual-lane P3D for throughput; offline pre-programming is supported so new products are prepared without stopping production (DaoAI-reported).
Decide 2D versus 3D from your defect Pareto, not from the demo. 3D adds height and volume measurement, which matters when your escapes are solder-volume defects: insufficient solder, lifted leads, coplanarity. If your pain concentrates in presence, wrong part, polarity, offset, and marking-driven false calls, a modern 2D system with AI classification covers the working set for less money. Neither answer is universally right; the Pareto is.
The height argument is real. A 2D image cannot directly measure solder volume, and on packages where the joint hides under the body, height data catches what grayscale cannot. If those defects are escaping today and costing you downstream, 3D earns its price.
The counterweight is that most high-mix false-call pain lives in the 2D domain: lot-to-lot appearance changes, same-color components, dense markings on inductors and crystals. Those are classification problems, and they respond to better judgment, not to height maps. Feature-based AI attacks them directly (the mechanics are in our false-call breakdown).
For transparency: DaoAI's P Series ships as 2D today, with a 3D version announced as coming soon. The buying advice stands regardless of whose machine you evaluate: list your actual escapes and false calls from the last quarter, then buy for that list.
Seven questions expose how an AOI will behave on a high-mix floor: what inputs programming requires, who runs a changeover and how long it takes, what happens with a never-seen component, how false calls decline over time, who maintains the component library, how criteria map to IPC-A-610, and how data reaches your MES. Ask every vendor the same seven and compare answers side by side.
For each, what a good answer sounds like:
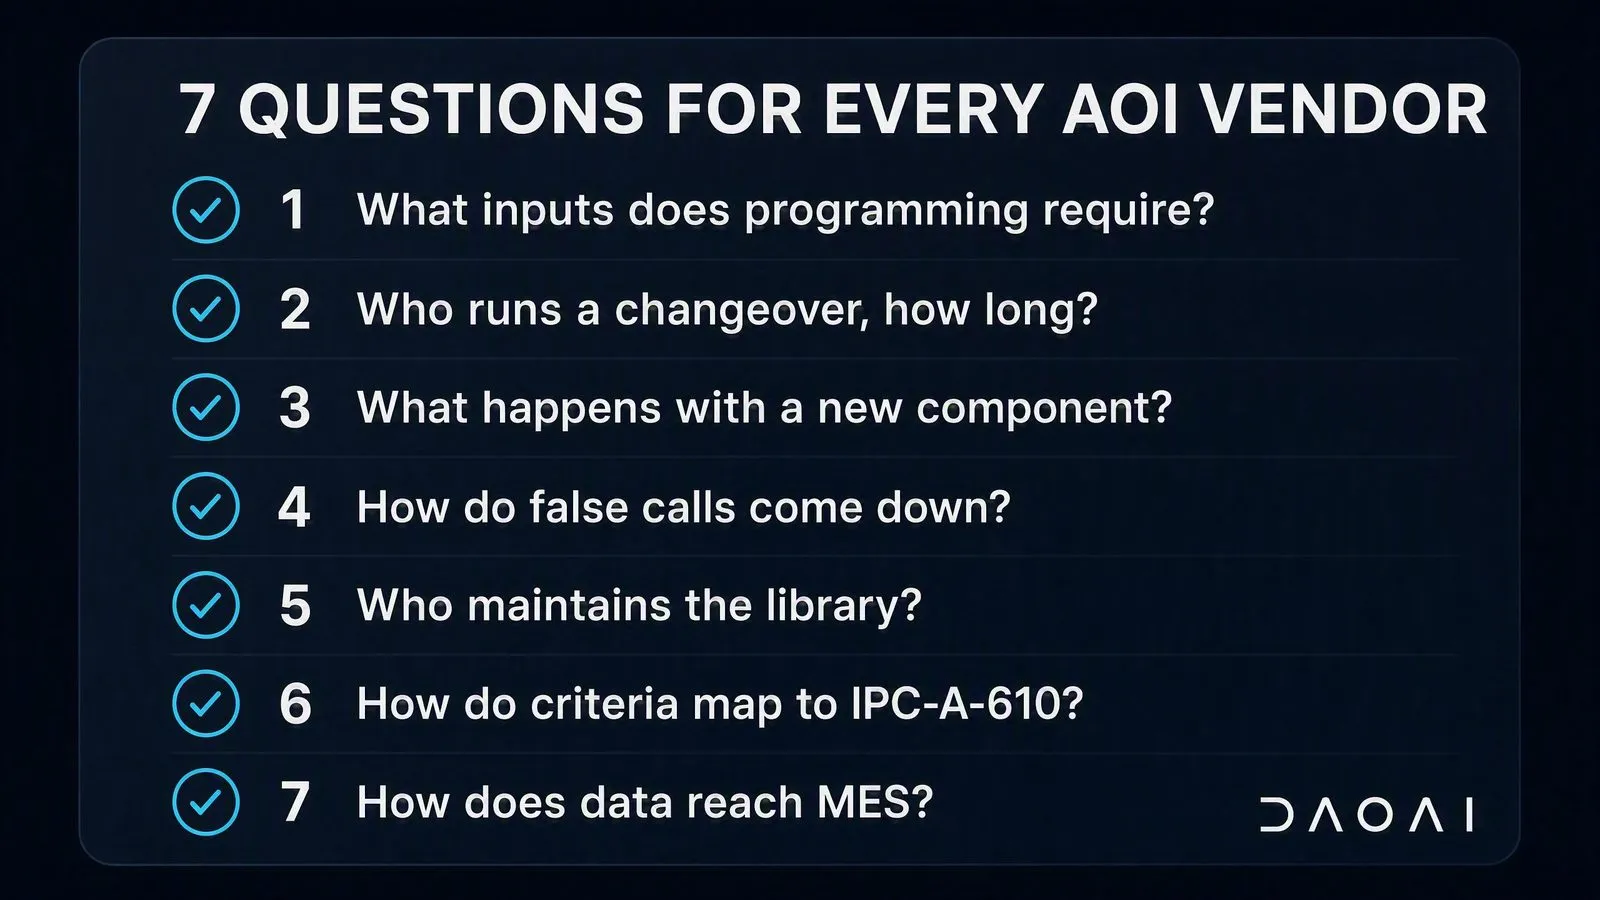
Ask us the same seven. A vendor who welcomes the list is telling you something; so is one who redirects to the camera specs.
Often, yes. If inspection can happen bench-side within your takt, an offline unit covers high-mix work at lower cost and with more flexibility. Inline becomes necessary when boards must be gated in line at rate, every pass. Many shops run offline for NPI and validation even after adding inline capacity for volume.
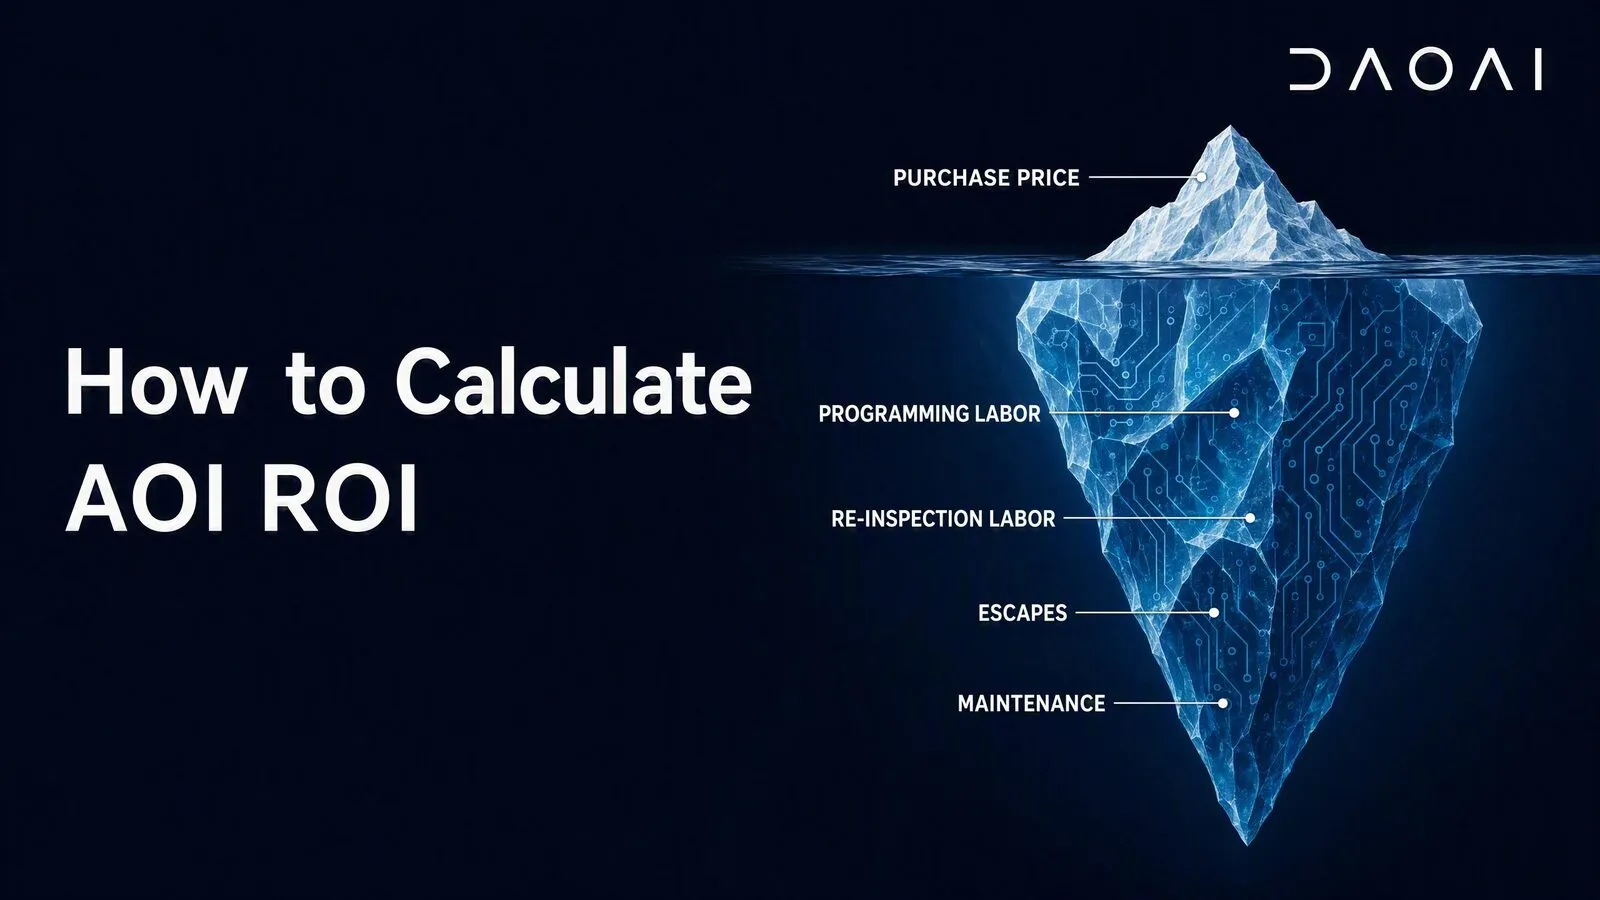
Vendors rarely publish list prices, and the sticker is the smaller part of the answer anyway. Total cost over five years is purchase price plus programming labor, re-inspection labor, and the cost of escapes. On a high-mix line the labor items usually outweigh the sticker: DaoAI estimates re-inspection and stoppage labor alone at 15,000 to 40,000 USD per operator per year on traditional systems (DaoAI-reported). Compare five-year totals, not quotes.
With offline pre-programming, yes in practice: new products are programmed and validated off the line while production runs, then inspection moves to whichever unit runs the job. A golden-board workflow helps here, since NPI boards often arrive before clean CAD data does.
Bring your worst boards, not your cleanest. Include a board with same-color components, one with marked inductors or crystal oscillators, and one for which you have no CAD data. Have your operator, not the vendor's engineer, run the changeover. Measure setup time and count false calls on your boards. An hour of that beats a day of slides.
If your six-question audit points at frequent changeovers and thin engineering coverage, weight the recurring column heavily and take the seven questions to every demo, ours included. DaoAI's P Series runs the golden-board workflow across offline (P1/P2) and inline (P3/P3D) units.
See how AOI identifies visible open solder joints, where fixed color thresholds struggle, and how a pretrained 2D model handles common and special cases.
September 17, 2026
Vendor ROI calculators decide the assumptions for you. Here is the whole model: eight cost lines, the formulas for false-call and escape savings, and two worked scenarios including one that does not pay.
August 25, 2026
Vendor accuracy numbers mean nothing until you reproduce them on your own boards. Six boards to bring, five things to measure, and what a passing result looks like.
August 11, 2026
AI inspection insights, product news, and industry analysis. Once a month, no noise.